Catalogue · The works
Runline Hydraulics is not one plant but several manufacturing sites in Zhuji, and each of them makes its own product. That specialisation gives a better ratio of price to quality than a single “do-everything” factory.
A ferrule, a flange and an adapter start from different blanks and need different machines and different regimes. A ferrule is best cold-headed from wire and then annealed in a furnace; a flange is forged and milled; an adapter is turned from bar on an automatic lathe with a bar feeder. A site that makes one thing sets up its machines, its people and its inspection for that one thing, and the part costs less than at a general-purpose plant where the same machines are re-tooled from ferrules to flanges.
For the buyer it looks like one catalogue and one contract: the order is consolidated at the warehouse in Zhuji and leaves in one container from Ningbo. Which site made which item is visible in the batch marking.
Five sites, five products

Ferrules
Crimp ferrules for braided, spiral and PTFE hose.
Cold heading from wire and bar, heat treatment after forming so that the ferrule flows under the press dies instead of cracking. Bore and wall thickness checked on every batch.

Small hose fittings
Studs and hose fittings from DN6 to DN25 — the largest part of the catalogue by volume.
Automatic lathes with bar feeders, CNC, round-the-clock operation. Threads and seat cones are gauged at every set-up.

Large hose fittings
Fittings from DN32 to DN51 and above, heavy elbows, special versions.
A separate site with larger machines and dies: large parts are not queued with mass-produced ones — that is expensive for both.

Flanges
SAE flange heads 3000 and 6000 psi, straight, 45° and 90°, and ISO 6162 flanges.
Die forging, milling and turning on machining centres, checks of the sealing-face flatness and the O-ring seat.

Adapters and tube connections
Adapters in every thread system of the catalogue and DIN 2353 bite-type couplings.
Bar work on multi-spindle automatics and CNC, forged elbow and tee bodies, full thread inspection across BSP, JIC, ORFS, metric and NPT.
Equipment and inspection
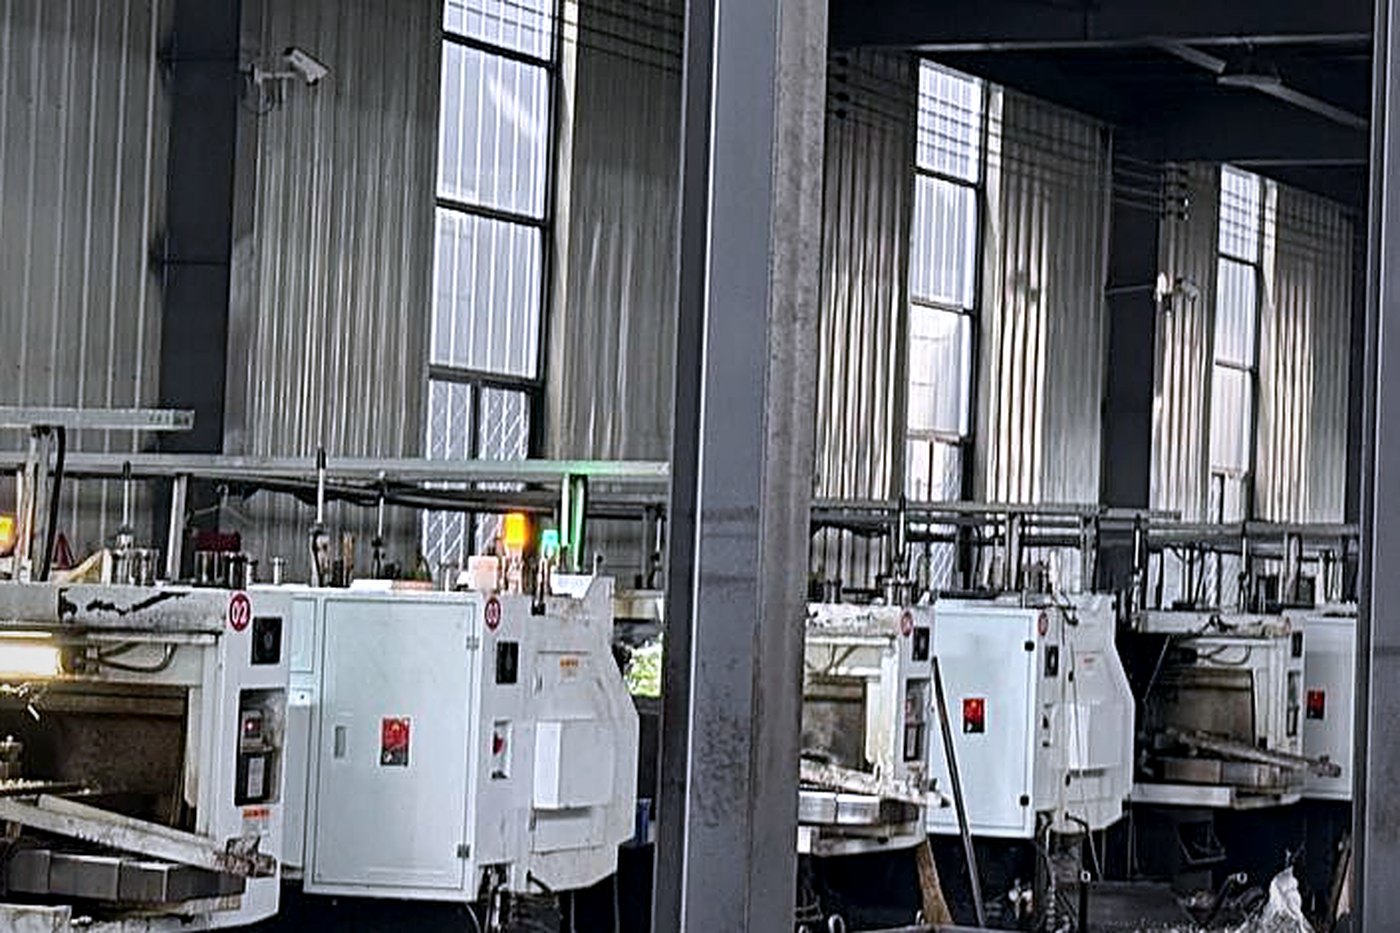
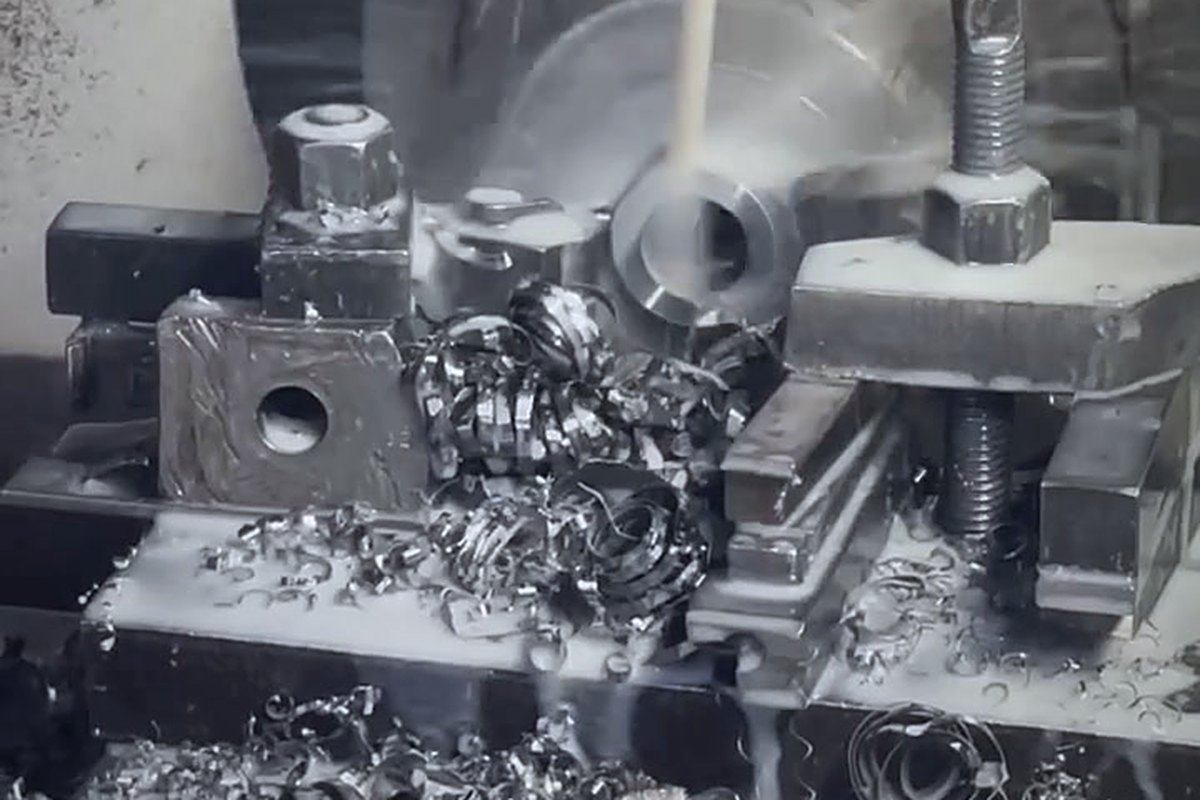
All sites run modern equipment: CNC lathes and mills, bar-fed automatics, cold-heading presses, heat-treatment furnaces and in-house zinc plating lines. Machines are renewed as series grow, not as they wear out.
Quality control is built at both ends. Incoming: the steel is checked — grade against the supplier certificate and sample chemical analysis, condition of bar and wire. Outgoing: every batch is checked for threads with gauges, dimensions against the drawing, coating thickness and salt-spray resistance on witness panels. Test reports are provided on request.
How the blanks are made, why ferrules are annealed and which steels the parts are made from is described in detail in the article “Manufacturing process”.
On the shop floor
Send us a parts list
A spreadsheet, a photo of a fitting, or a page from a competitor's catalogue. We come back with prices, carton quantities and how it fills a container.